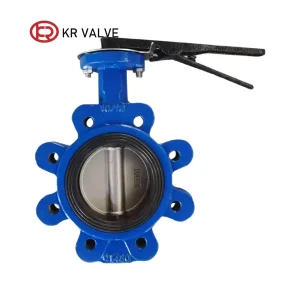
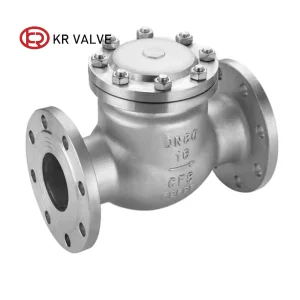
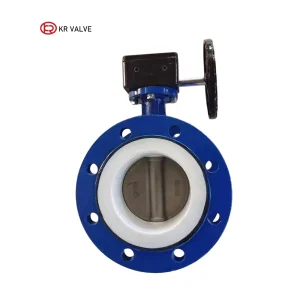
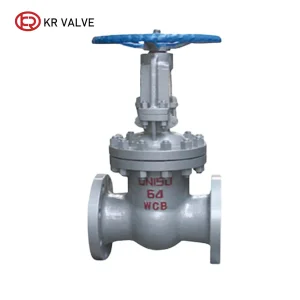
Engineered to international specifications, optimized for local water management and heavy industrial applications.
Navigating municipal modernization, strict environmental compliance, and high-performance engineering specifications.
New Amsterdam stands as a dynamic nexus of municipal growth, commercial enterprise, and advanced infrastructural frameworks. As regional utilities and municipal networks undergo continuous modernization, the demand for high-reliability flow control systems has surged exponentially. Industrial facilities, water treatment plants, and commercial complexes across the area require robust, corrosion-resistant, and precision-engineered valve systems to maintain uninterrupted operations under high-pressure parameters.
From legacy pipeline retrofitting to greenfield smart city expansion, project engineers and procurement directors in New Amsterdam constantly seek resilient supply chain partners who can bridge the gap between rigorous local standards and cost-efficient manufacturing capabilities.
Procuring industrial components for New Amsterdam installations demands absolute adherence to statutory standards and international certifications (ISO, DIN, BS, ANSI). Our manufacturing infrastructure ensures that every valve exported to the region meets or exceeds local pressure vessel directives, potable water safety certifications (such as WRAS/NSF compliance equivalents), and environmental zero-leakage mandates.
We provide comprehensive documentation, material test reports (MTR), and dedicated technical consulting to ensure frictionless customs clearance and seamless integration into existing New Amsterdam municipal grids.
Combining 20+ years of manufacturing expertise with agile logistics and unmatched cost efficiency.
Equipped with over 15 high-precision CNC machining centers, automatic assembly lines, and rigorous in-house spectral analysis laboratories to guarantee zero defects.
Offering over 500 valve varieties across 20 core series, supporting full OEM/ODM branding services tailored for global distributors and regional contractors.
Streamlined export logistics ensuring safe, trackable, and timely delivery to over 50 countries and regions worldwide, meeting strict project milestone deadlines.
The global valve manufacturing sector is shifting rapidly toward intelligent automation, smart actuator integration, and ultra-durable eco-friendly sealing materials (such as EPDM, PTFE, and specialized stainless steel overlays). In New Amsterdam applications—spanning sewage treatment, seawater desalination, dam construction, and natural gas distribution—operational downtime carries a prohibitive cost.
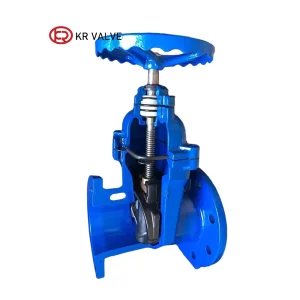
By investing in high-grade ductile iron gate valves, precision butterfly valves, and specialized Y-type strainers, asset owners ensure decades of maintenance-free service life, maximizing ROI and minimizing environmental risk.
Backed by decades of field-tested reliability across diverse international infrastructure projects.
With over 20 years of dedicated specialization in standard and custom valve manufacturing, KR VALVE has earned an exemplary reputation for repeat orders and long-term industrial partnerships. Our technical team works relentlessly on continuous product innovation, rigorous hydrostatic pressure testing, and responsive 24-hour pre-sales and post-sales consultancy.
Expert answers to critical procurement, technical, and logistical inquiries for New Amsterdam buyers.
Explore our extensive range of butterfly valves, gate valves, check valves, and filtration systems.
 KR VAVLE