Explore our premium selection of certified industrial valves, engineered for extreme reliability and precise flow management.
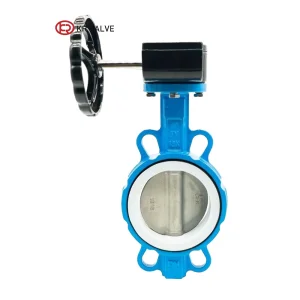
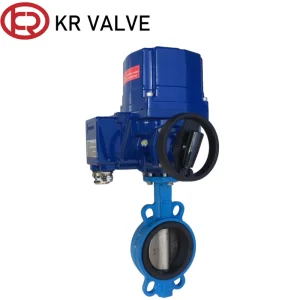
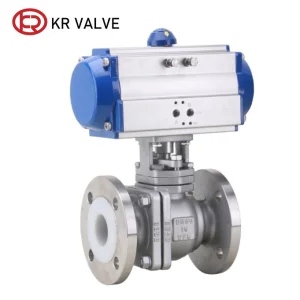
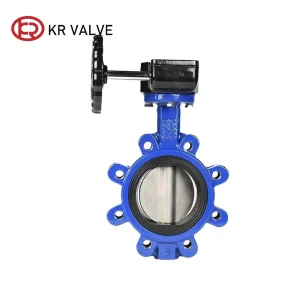
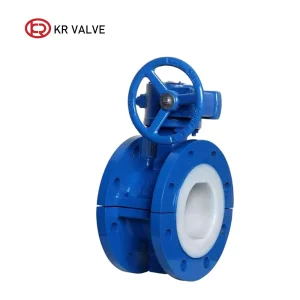
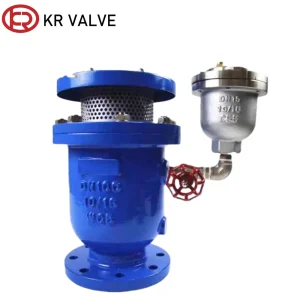
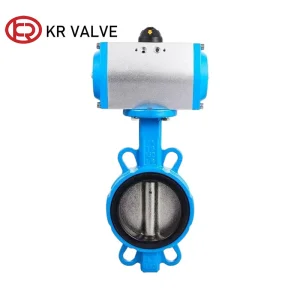
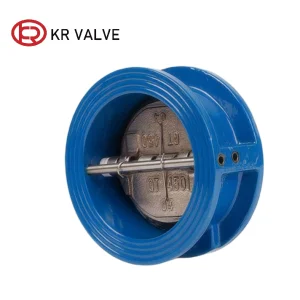
As a leading authority in the industrial valve manufacturing sector, KR VALVE combines decades of technical mastery with rigorous quality control frameworks to power global fluid networks.
KR has more than 20 years of experience in producing standard and non-standard valves of various types. We supply a wide selection of over 500 valve products, including butterfly valves, gate valves, check valves, water control valves, and all matching accessories. These products have critical applications in various industries such as water treatment, dam construction, commercial buildings, energy and heating, and chemical engineering. We have won high repeat purchase rates from customers with excellent product variety and quality.
Beyond product excellence, we are dedicated to creating a mutually beneficial partnership with every customer. We believe that reliable service is as crucial as superior products, striving to continuously optimize the customer experience to achieve long-term win-win cooperation.
Today, KR VALVE’s products have been exported to over 50 countries and regions in Europe, Asia, Africa, and Oceania, providing project construction and brand marketing services to thousands of customers. We look forward to collaborating with you, leveraging our expertise, comprehensive product range, and unwavering commitment to quality and service to support your success.
Our operational framework strictly adheres to international standards (ISO-9001, DIN, ANSI, BS), guaranteeing zero leakage and maximum structural integrity under extreme operating pressures and corrosive environments.
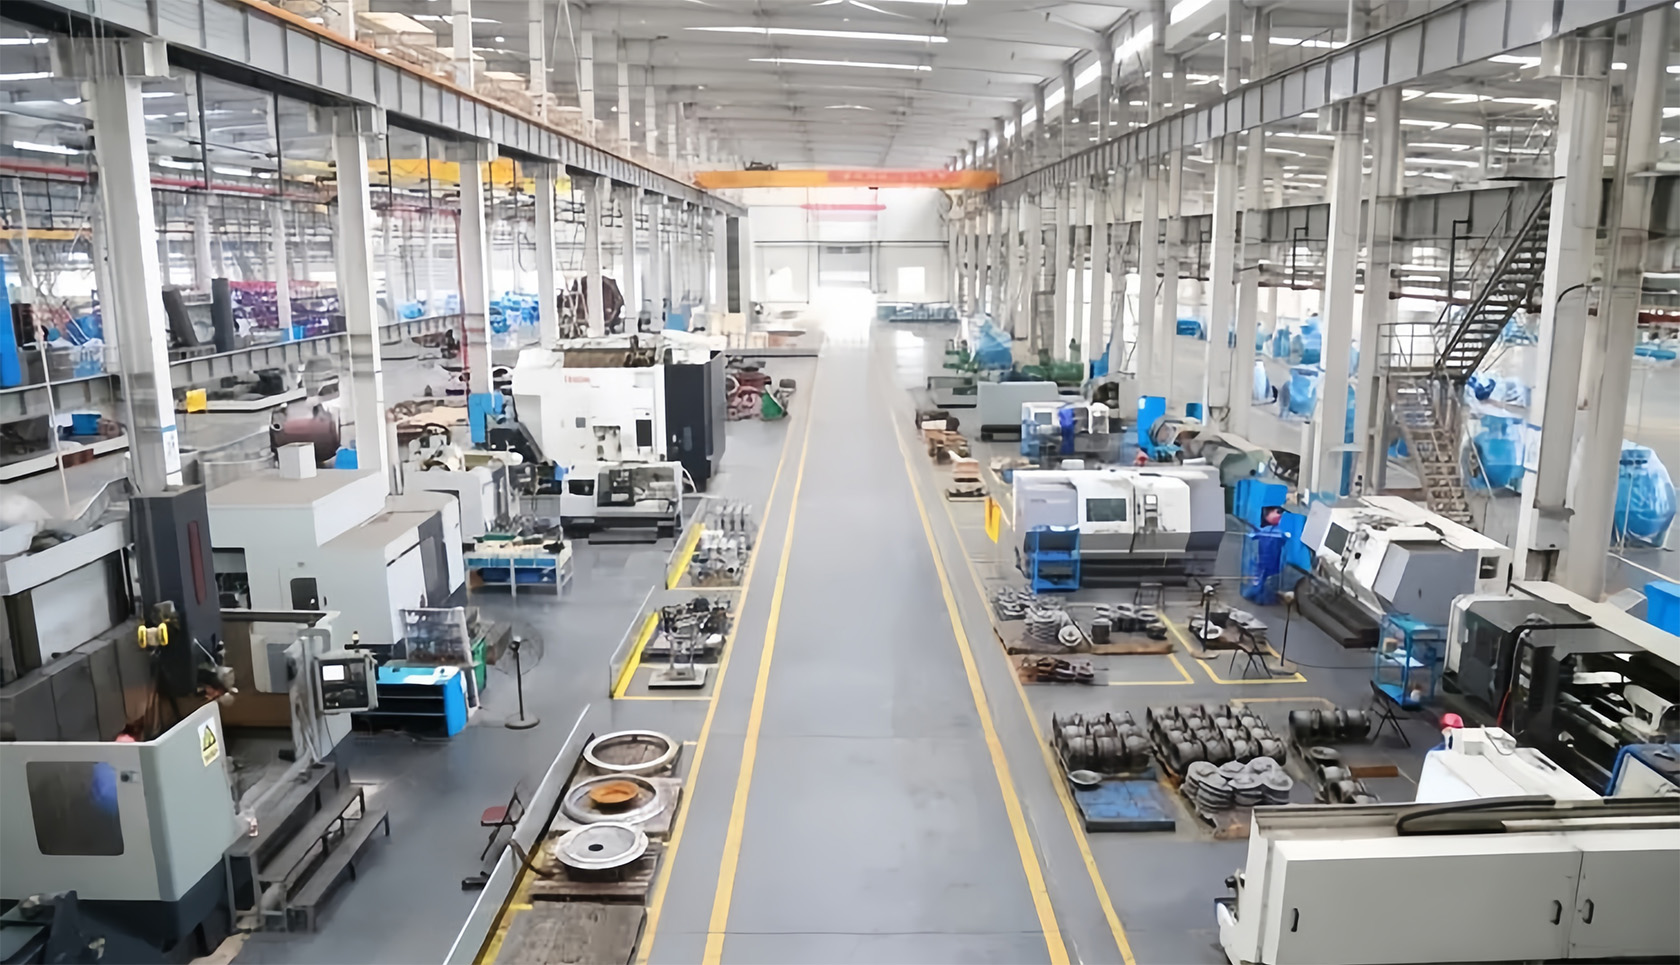
Our end-to-end manufacturing process ensures absolute precision, compliance, and zero-defect delivery.
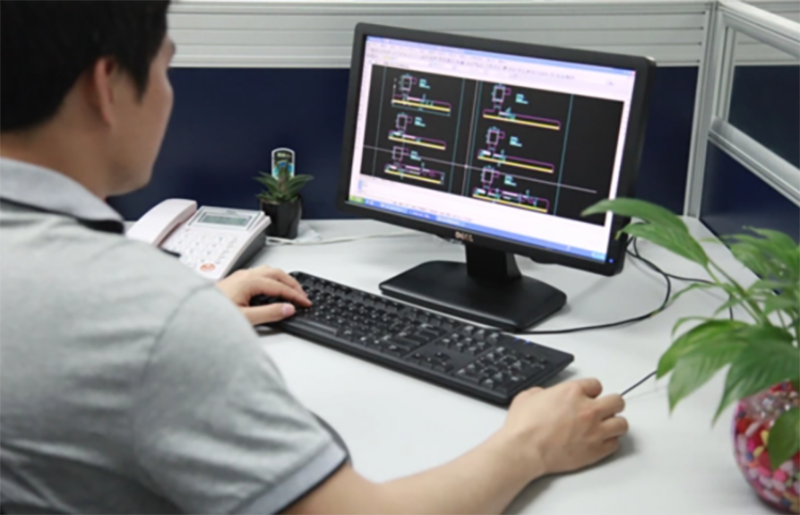
Our dedicated R&D department ensures continuous product design and innovation. Our technicians continuously design and develop products meeting strict customer and market requirements. Our laboratory provides modern testing capabilities to elevate product performance, encompassing 20 series and over 500 product varieties.
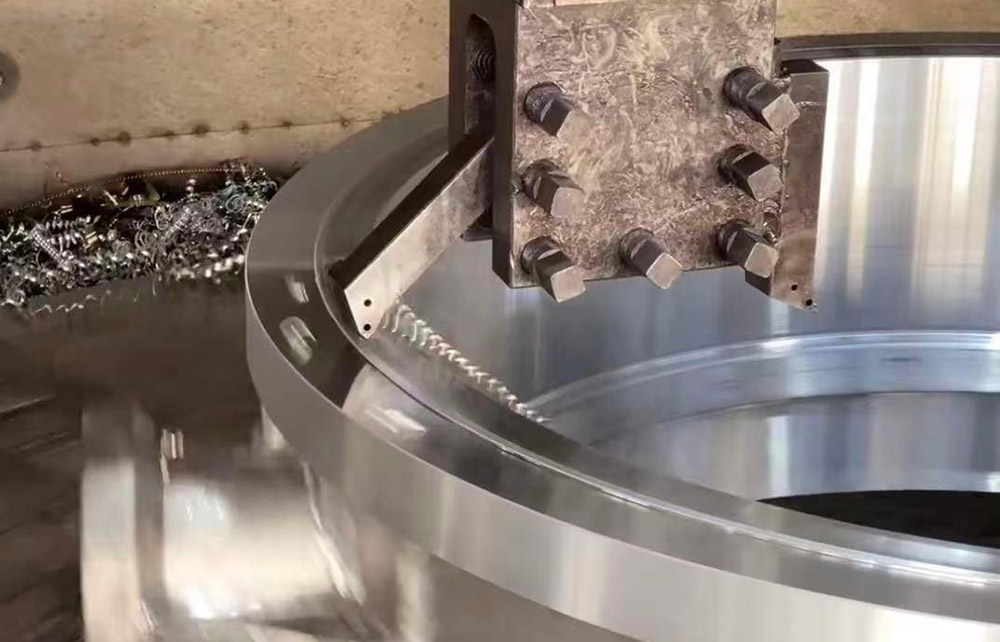
The production department formulates optimized manufacturing schedules, executing production under strict ISO-9001 quality management supervision. Equipped with over 30 advanced production machines and monthly inventory adjustments, we consistently exceed client expectations for rapid delivery timelines.
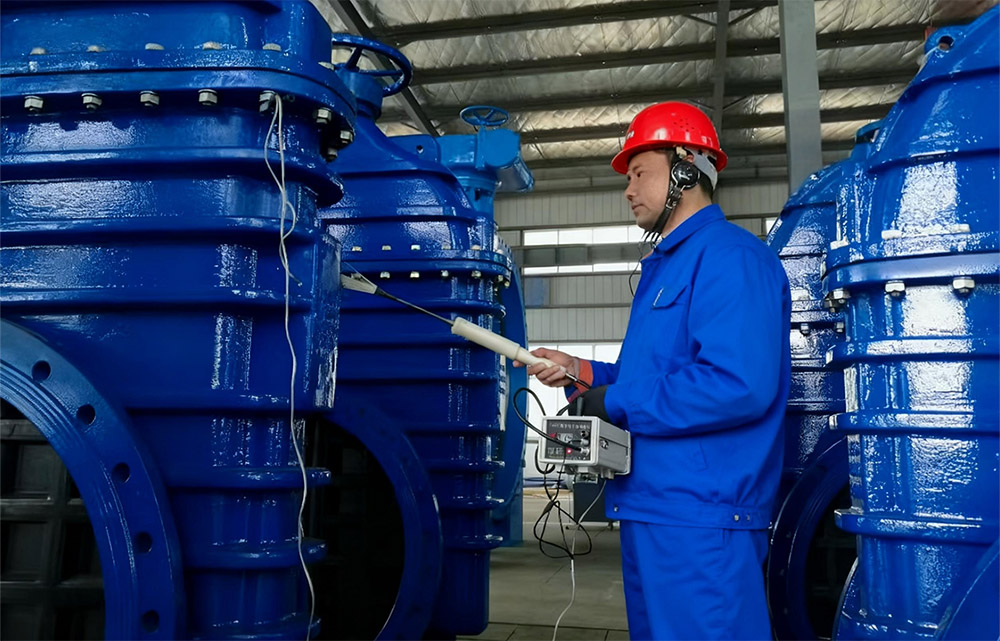
Our quality inspection department ensures 100% inspection coverage. Zero leakage is our core manufacturing principle. Following strict international standards, we execute comprehensive appearance, dimensional, and hydrostatic pressure tests, issuing fully compliant inspection certificates.
A deep-dive whitepaper analysis into current commercial realities, localization dynamics, and next-generation flow control advancements.
The international valve manufacturing market is undergoing a structural evolution driven by accelerating urbanization, massive investments in water resource management, and stringent industrial emission regulations. Custom check valves and heavy-duty industrial valves are the cornerstone of fluid protection systems, preventing catastrophic backflow and water hammer phenomena in municipal water treatment, petrochemical plants, and cross-border fluid transportation pipelines.
Global supply chains increasingly demand custom manufacturing capabilities (OEM/ODM), where standardized off-the-shelf components no longer suffice for complex engineering projects. Factories capable of tailoring body materials (such as Ductile Iron, WCB, CF8, Stainless Steel) and internal seat configurations (PTFE, EPDM) dominate market share.
Looking toward 2030, the industrial valve sector is pivoting towards smart automation, IoT-enabled predictive maintenance, and eco-friendly materials. Key milestones on the industry technology roadmap include:
Our comprehensive service matrix guarantees uncompromised value across price, quality, and technical support.
We manage our independent global brand ‘KR’ while providing robust OEM and ODM manufacturing services, building long-term relationships with premier international brands.
Equipped with 15 specialized machining lines and state-of-the-art assembly bays, operated by highly trained, certified industry artisans.
Offering over 20 distinct product series and 500+ commercial varieties, satisfying both international standards and highly specific non-standard customizations.
Every individual component undergoes meticulous dimensional and metallurgical inspection prior to final assembly into a flawless finished product.
By independently controlling every stage of internal manufacturing, raw material sourcing, and assembly, we deliver exceptional pricing advantages.
Comprehensive pre-sales technical consultation and rapid-response after-sales engineering support delivered by industry experts.
Proven real-world deployments of KR industrial valves across complex municipal and heavy industrial environments worldwide.
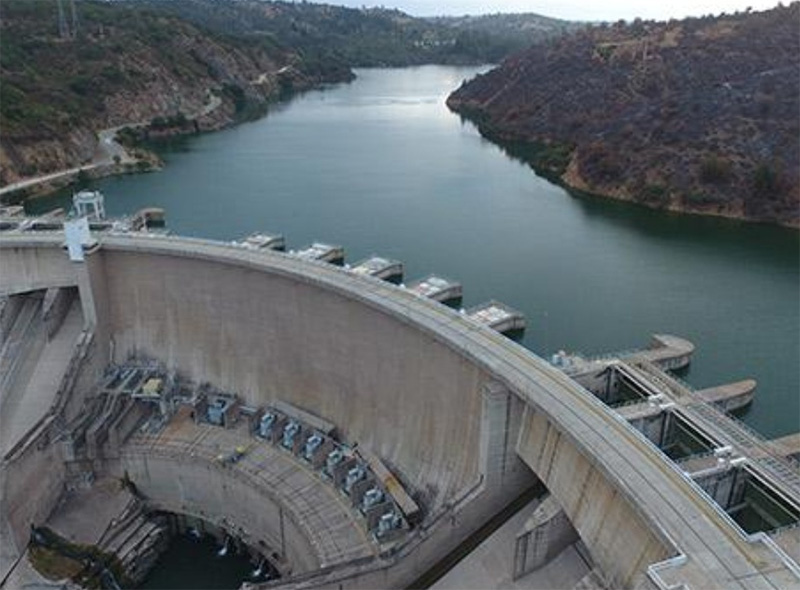
KR supplied specialized high-pressure water control valves and custom check valves to major national dam construction initiatives in Chile, ensuring fail-safe flow regulation under extreme hydrostatic pressure.
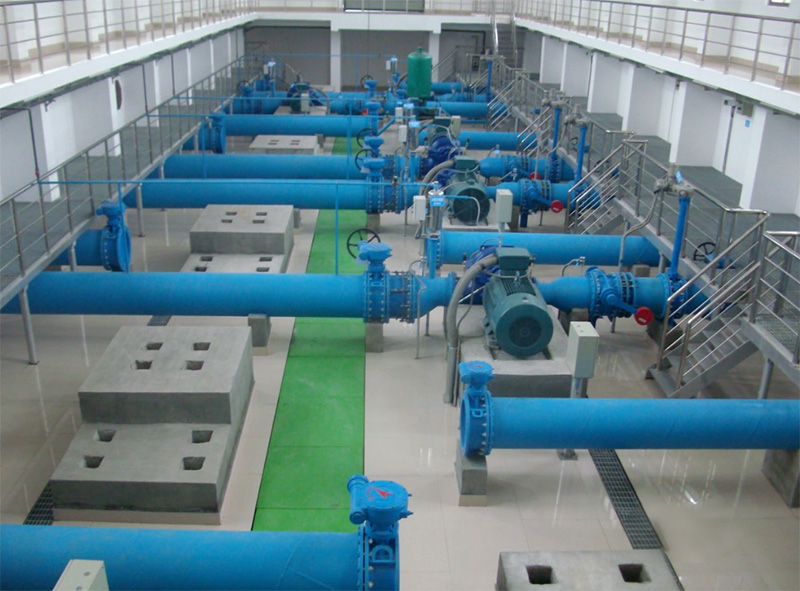
Delivered large-diameter butterfly valves and resilient seated check valves for municipal water treatment infrastructure upgrades across northern Italy, satisfying rigorous EU environmental standards.
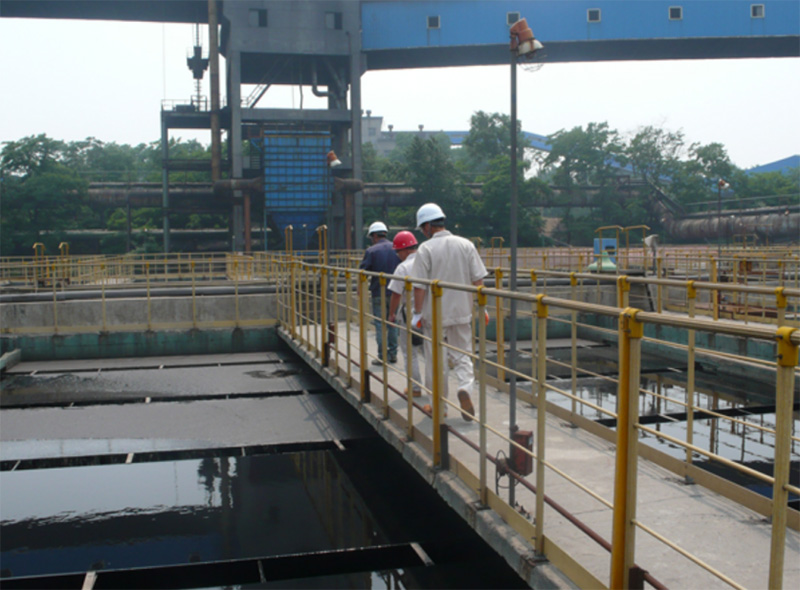
Provided comprehensive corrosion-resistant valve packages, including specialized check valves and gate valves, empowering municipal wastewater treatment facilities in metropolitan Brazil.
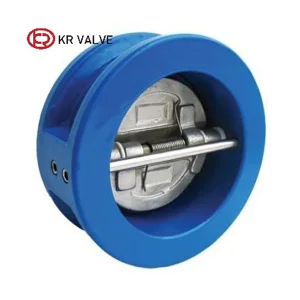
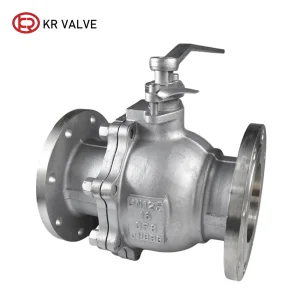
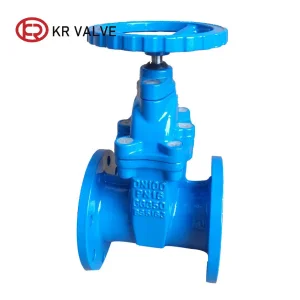
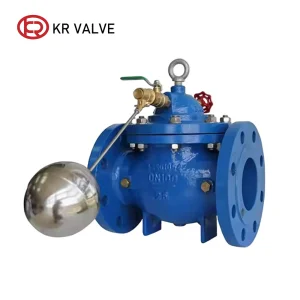
Discover our extended catalog of precision-engineered valve solutions ready for global dispatch and OEM customization.
Expert answers regarding custom check valves, manufacturing standards, and global supply chain partnerships.
With over 20 years of specialized metallurgical and flow control expertise, KR VALVE provides rigorous ISO-9001 certified manufacturing, 100% zero-leakage hydrostatic testing, and bespoke engineering designs tailored to unique industrial parameters.
Yes. We support comprehensive OEM/ODM manufacturing partnerships, supplying independent brand packaging, custom body materials (Ductile Iron, WCB, Stainless Steel), and specialized seat linings (PTFE, EPDM).
Our valves are widely deployed in municipal water treatment, commercial dam construction, chemical processing plants, oil and natural gas pipelines, and large-scale HVAC energy heating systems.
Thanks to our robust inventory management and 15 advanced machining lines, we maintain rapid production cycles. We have successfully exported our products to over 50 countries across Europe, Asia, Africa, and Oceania.
 KR VAVLE