Explore our primary industrial ball valve line engineered to ISO, ANSI, and DIN standards for maximum operational reliability in Grenville.
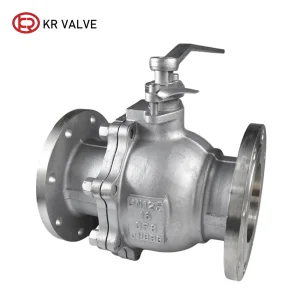
The industrial and commercial sector serving Grenville is undergoing a major technological transformation. As regional municipal water treatment, commercial HVAC automation, agricultural processing, and specialized chemical distribution systems expand, the demand for precision-engineered fluid control components has escalated significantly. Modern infrastructure projects across the Grenville area mandate rigorous valve performance to prevent downtime, reduce maintenance overhead, and guarantee zero-leakage security under fluctuating pressure profiles.
Ball valves serve as the foundational backbone of these critical fluid lines. Whether governing high-pressure clean water supply networks or handling corrosive chemical slurries, selecting the right manufacturing partner is paramount for engineers, procurement officers, and EPC contractors in Grenville.
Key Insight: Grenville's evolving environmental regulations require industrial valves to comply with low fugitive emission standard ISO 15848-1 alongside API 6D pressure testing parameters.
Bridging direct factory pricing with world-class metallurgic casting, advanced CNC precision machining, and strict international quality assurance.
Utilizing investment casting (lost-wax process) for CF8 (304) and CF8M (316) stainless steel components ensures dimensional accuracy, minimal surface roughness, and superior structural integrity under thermal stress.
Direct sourcing from OEM valve factories eliminates regional distributor markups, allowing Grenville contractors to achieve up to 35% cost reduction without compromising material certifications.
Every single valve undergoes 100% shell hydrostatic testing and high-pressure seat leakage tests compliant with API 598 standards prior to export dispatch.
Understanding the engineering distinctions between valve configurations to optimize selection for Grenville application requirements.
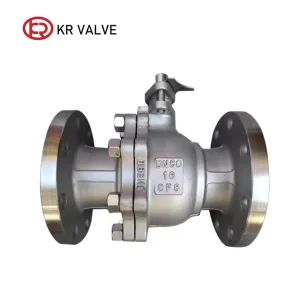
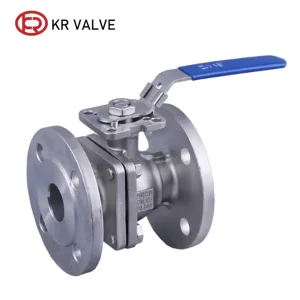
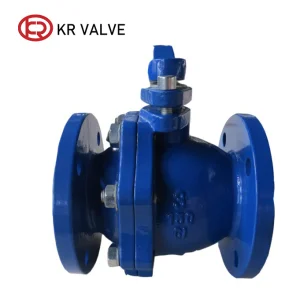
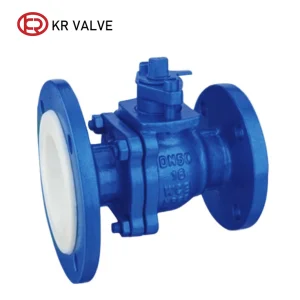
| Feature Parameter | Floating Ball Valves | Trunnion-Mounted Ball Valves | PTFE-Lined Corrosion Resistant Valves |
|---|---|---|---|
| Pressure Rating | Class 150 - Class 600 (PN10 - PN100) | Class 150 - Class 2500 (Up to PN400) | Class 150 / PN10 - PN16 |
| Seating Mechanism | Upstream pressure pushes ball onto downstream seat | Spring-loaded seats push against fixed ball | Virgin PTFE / PFA encapsulated elastomer |
| Target Media | Clean fluids, water, steam, light oil | High-pressure gas, crude oil, heavy slurry | Aggressive acids (HCl, H2SO4), alkaline media |
| Grenville Suitability | Municipal water supply & standard HVAC | Industrial gas pipelines & energy storage | Chemical treatment plants & paper processing |
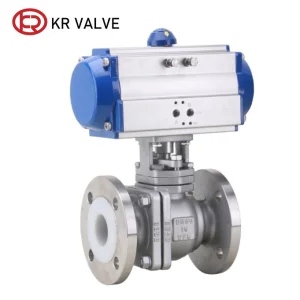
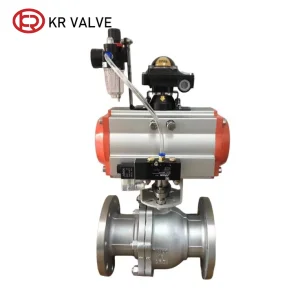
Modern industrial operations in Grenville require dynamic automated flow regulation. Our manufacturing facilities produce fully integrated automated packages including:
KR has more than 20 years of experience in producing standard and non-standard valves of various types. We supply a wide selection of over 500 valve products, including butterfly valve, gate valve, check valve, water control valve, as well as all their matching and accessory products.
These products have applications in various industries such as water treatment, dam construction, commercial buildings, energy and heating, chemical engineering, etc. We have won high repeat purchase rates from customers with excellent product variety and quality.
Beyond product excellence, we are dedicated to creating a mutually beneficial partnership with every customer. We believe that reliable service is as crucial as superior products, and we strive to continuously optimize the customer experience to achieve long-term win-win cooperation. Today, KR VALVE’s products have been exported to over 50 countries and regions in Europe, Asia, Africa, and Oceania, providing project construction and brand marketing services to thousands of customers.
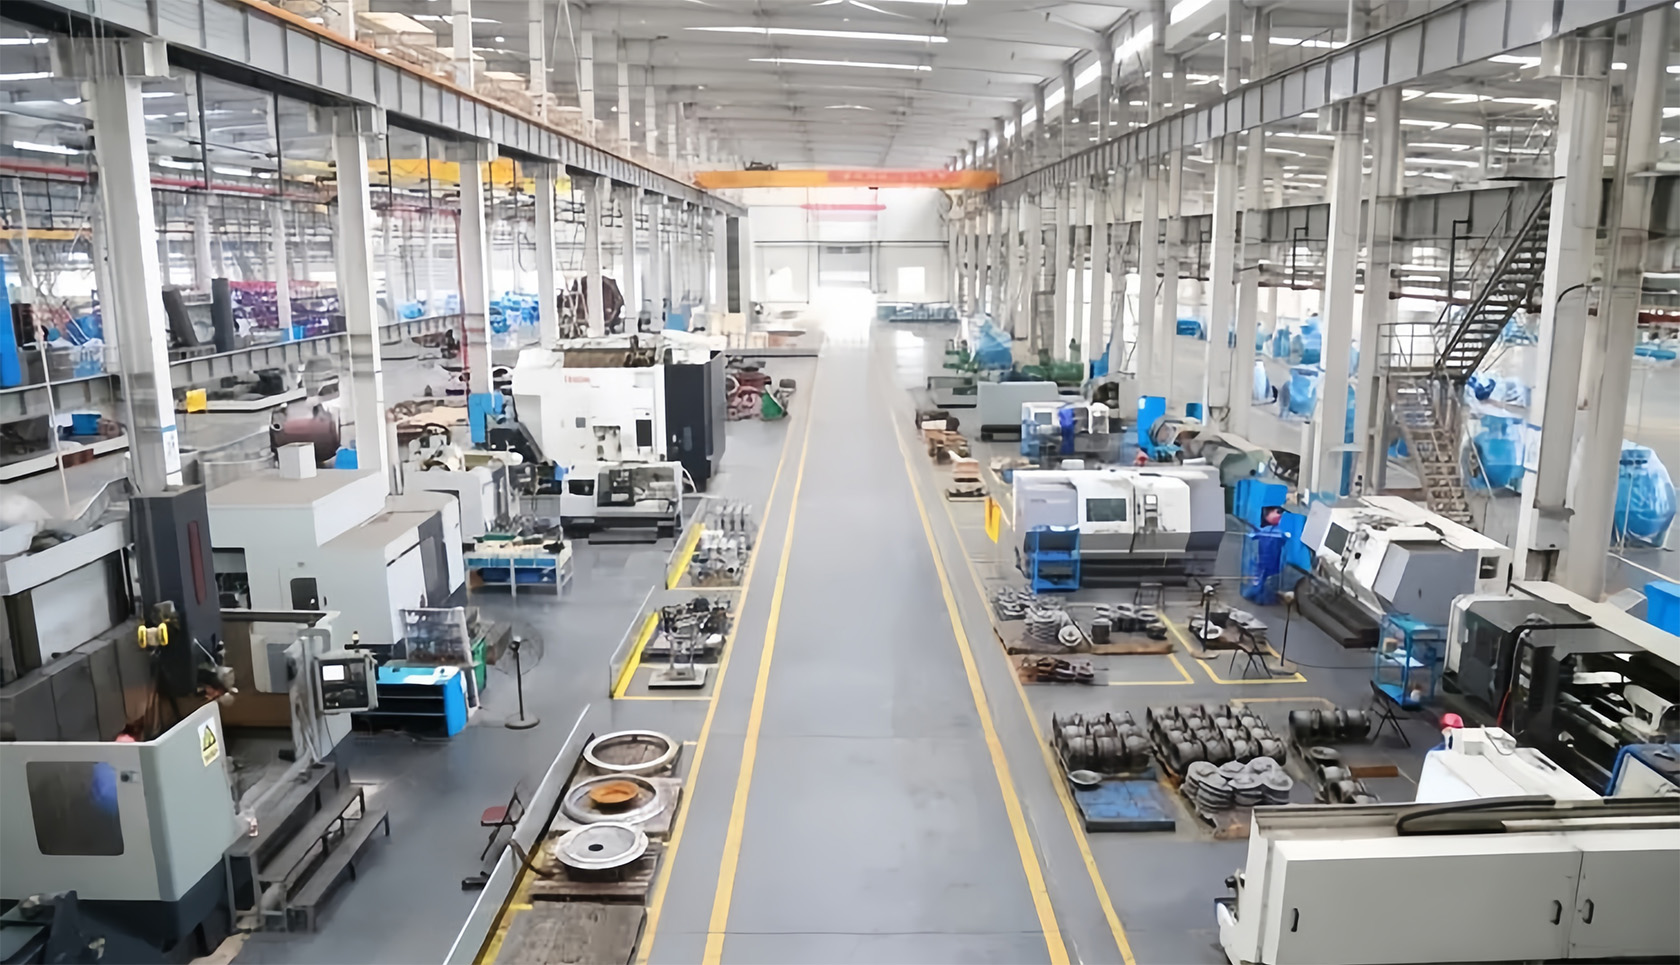
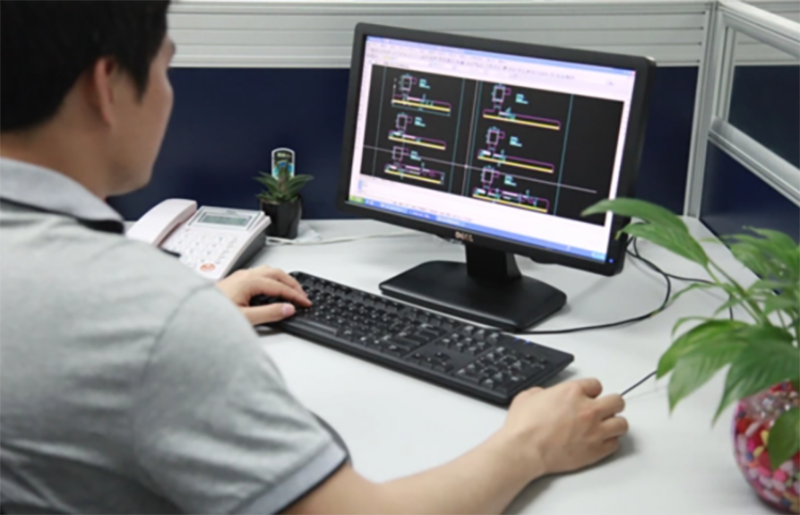
R&D department ensures continuous innovation. Technicians design and develop products meeting specific market requirements. Modern lab capabilities elevate performance across 20 series and 500+ varieties.
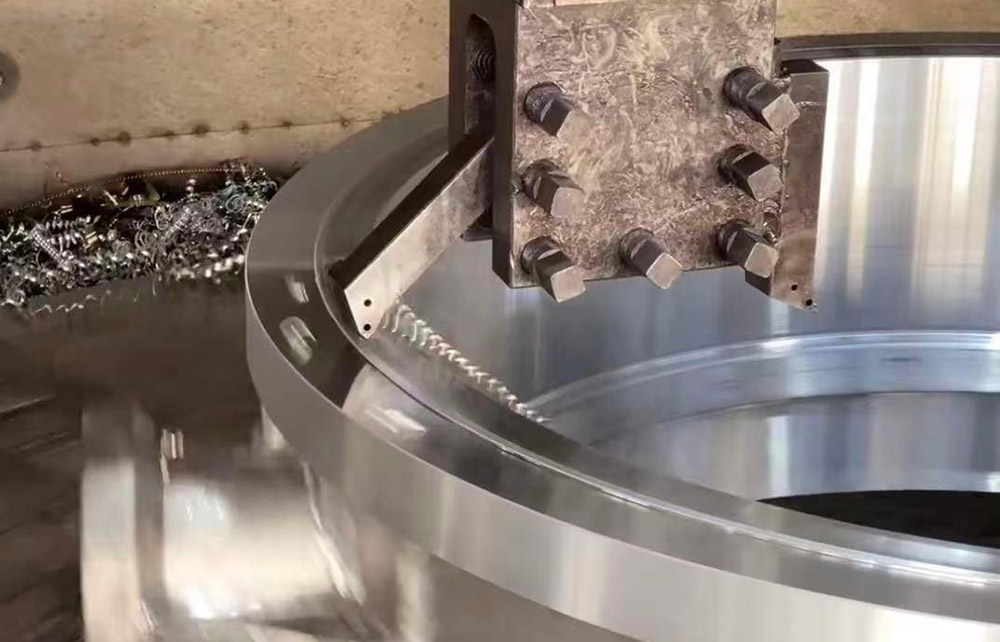
Production plans ensure timely delivery under strict ISO-9001 supervision. Equipped with 30+ advanced machining setups to exceed expectations on complex orders.
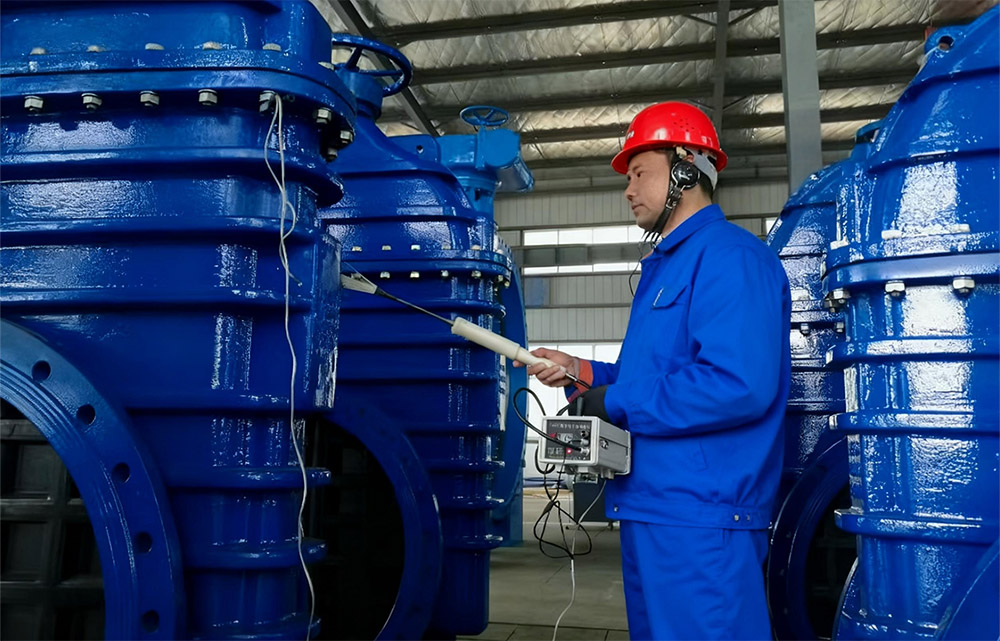
Zero leakage is our core principle. Inspection protocols test appearance, dimension, hydrostatic, and pneumatic pressure, complete with certified test reports.
Proving quality and endurance across demanding international civil and industrial deployments.
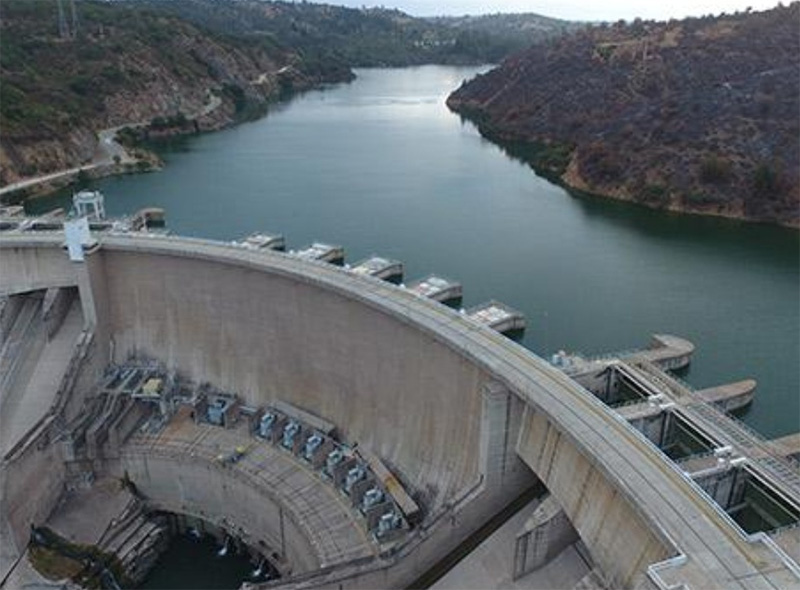
Supplied heavy-duty custom water control valves built for extreme hydraulic pressures in hydro-infrastructure works.
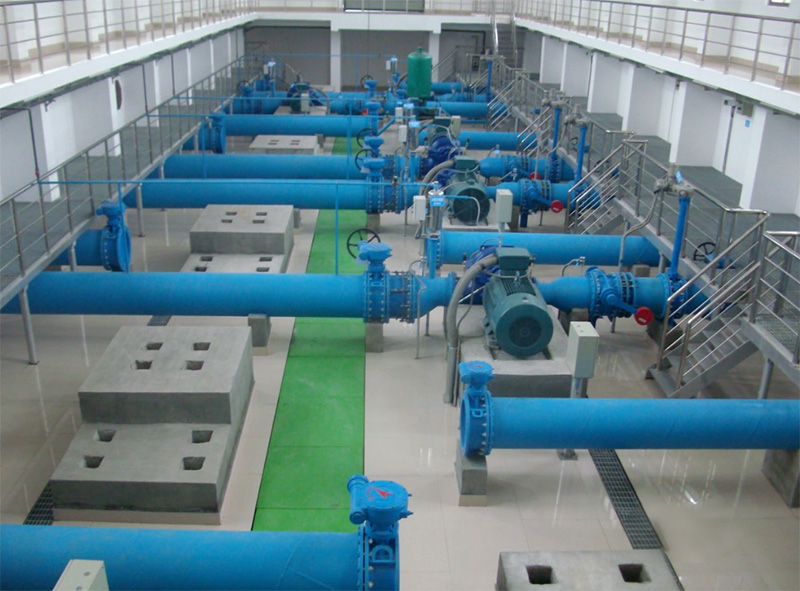
Delivered large-diameter butterfly and non-return check valves for regional municipal water networks.
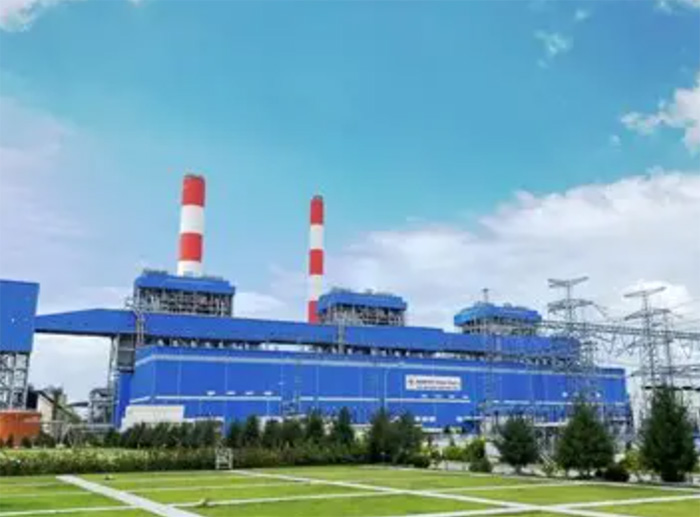
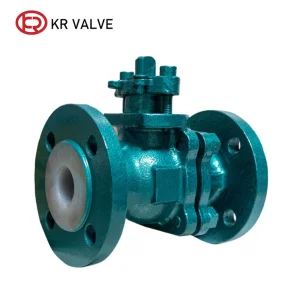
Engineered full PTFE-lined corrosion-resistant ball valves for aggressive acid distribution systems.
Expert technical insights regarding valve specification, material selection, and factory sourcing for Grenville projects.
Browse our complete series of industrial ball valves, check valves, and automatic release systems engineered for the Grenville market.
Partner directly with an industry-leading OEM valve manufacturer. Get immediate factory pricing, comprehensive CAD designs, and tailored technical support today.
Send Inquiry Now KR VAVLE